

api 5l x46 pipe specification-ssaw
group nameAPI 5L Spiral Welded Line Pipe – SSAW for Oil & Gas Transmission
-
Min Order5 ton
brand nameCangzhou Spiral Steel Pipe Manufacturers
modelAPI 5L X46 SSAW Pipe
payment methodL/C, T/T
-
update timeSun, 27 Sep 2026 14:42:35 GMT
Paramtents
TRADE TERM FOB CFR CIF
Standard API 5L ISO3183
Technique SSAW
Grade X46 (Q, M, QS, MS) , L320
Processing Service Welding, Punching, Cutting, Bending, Decoiling
Length 12M, 6m, 6.4M Up to 30 meters in length
Certificate API, CE, EN10210, EN10219, DIN, JIS, BV, ISO9001
Ends 1.Plain End2. Beveled3.Threaded.4 Screwed
Outer Diameter up to 144”
Packging & Delivery
Min Order5 ton
Briefing
API 5L X46 pipe is a low to medium grade pipe material that meets the API 5L standard, also known as L320 pipe. These welded pipes have a minimum yield strength of 320 Mpa (46400 psi). The minimum tensile strength is 435 Mpa.
Detailed
API 5L X46 pipe is a low to medium grade steel pipe that meets the API 5L standard, also known as L320 pipe. Its minimum yield strength is 320 MPa (46400 psi) and minimum tensile strength is 435 MPa. This steel grade covers two manufacturing types: seamless pipes and welded pipes (ERW, SAW), and is widely used in the field of oil and gas transportation.
Among them, the API 5L X46 SSAW pipe is manufactured using the Spiral Sub submerged Arc Welding process, covering two specification levels: API 5L PSL1 and API 5L PSL2, and including PSL2 material suitable for acidic environments.
Cangzhou Spiral Welded Steel Pipe Manufacturing Group relies on 13 production lines, CNAS accredited testing centers, and complete pipeline specifications to provide one-stop spiral welded pipe production, customized processing, and inspection services, which can meet the full process requirements of API 5L X46 and other steel grade pipelines from manufacturing to testing.
Pipeline Delivery Type
| Steel Grade | Applicable Standards | Delivery Terms | Applicable Scenarios | Meaning of Suffix Letters |
| API 5L X46 PSL1 | API 5L PSL1 | hot rolling | General delivery conditions | - |
| API 5L X46N/M/Q | API 5L PSL2 | N、 M、Q | Conventional PSL2 pipeline | N: Normalizing after rolling, normalizing after forming, normalizing; M: Thermal mechanical rolling or thermal mechanical forming; Q: Quenching and tempering |
| API 5L X46NS/MS/QS | API 5L PSL2 | N、M、Q + S | PSL2 pipeline with acidic medium | S: Sulfur containing service (acidic environment) |
Welding Characteristics
The API 5L X46 spiral welded steel pipe you mentioned has a minimum yield strength of 46400 pounds per square inch or 320 megapascals. The X46 spiral welded steel pipes you can currently see belong to controlled microalloyed carbon manganese steel. The main alloying elements are Nb, V, and Ti, and the total content of the microalloy does not exceed 0.15%. Therefore, you can see that the structure of this type of pipe is composed of needle like ferrite and bainite, which usually have good welding performance.
Advantages of API 5L X46 SSAW Pipe
a. Higher intensity than Class B and X42.
b. High resistance to dynamic tearing
c. High and low temperature impact toughness
d. Low ductile brittle transition temperature
e. Applicability to acidic environments, suitable for NACE
f. Economical and durable
Its excellent performance is attributed to the ultra-low carbon needle like ferrite structure, where high-density dislocations interact with small precipitates.
API 5L X46 SSAW Pipe Specification
API 5L pipeline data sheet, other grade specifications in API 5L, can be downloaded if needed.
API 5L X46 PSL1 Chemical and Mechanical Properties
| Chemical composition for API 5L PSL1 pipe Wall thickness ≤ 25.0 mm (0.984 in) | ||||||||
| Chemical Composition | ||||||||
| Steel Grade Steel Name | Wall Thickness ≤ 25.0 mm (0.984 in) | |||||||
Mass fraction, based upon heat and product analyses | ||||||||
% | ||||||||
C | Mn | P | S | V | Nb | Ti | ||
max | max | min | max | max | max | max | max | |
Welded Pipe(SSAW) | ||||||||
L175 Or A25 | 0.21 | 0.6 | - | 0.030 | 0.030 | - | - | - |
L175P Or A25P | 0.21 | 0.6 | 0.045 | 0.080 | 0.030 | - | - | - |
L210 Or A | 0.22 | 0.9 | - | 0.030 | 0.030 | - | - | - |
L245 Or B | 0.26 | 1.2 | - | 0.030 | 0.030 | c,d | c,d | d |
L290 Or X42 | 0.26 | 1.3 | - | 0.030 | 0.030 | d | d | d |
L320 Or X46 | 0.26 | 1.4 | - | 0.030 | 0.030 | d | d | d |
L360 Or X52 | 0.26 | 1.4 | - | 0.030 | 0.030 | d | d | d |
L390 Or X56 | 0.26 | 1.4 | - | 0.030 | 0.030 | d | d | d |
L415 Or X56 | 0.26 | 1.4 | - | 0.030 | 0.030 | f | f | f |
L450 Or X65 | 0.26 | 1.45 | - | 0.030 | 0.030 | f | f | f |
L485 Or X70 | 0.26 | 1.65 | - | 0.030 | 0.030 | f | f | f |
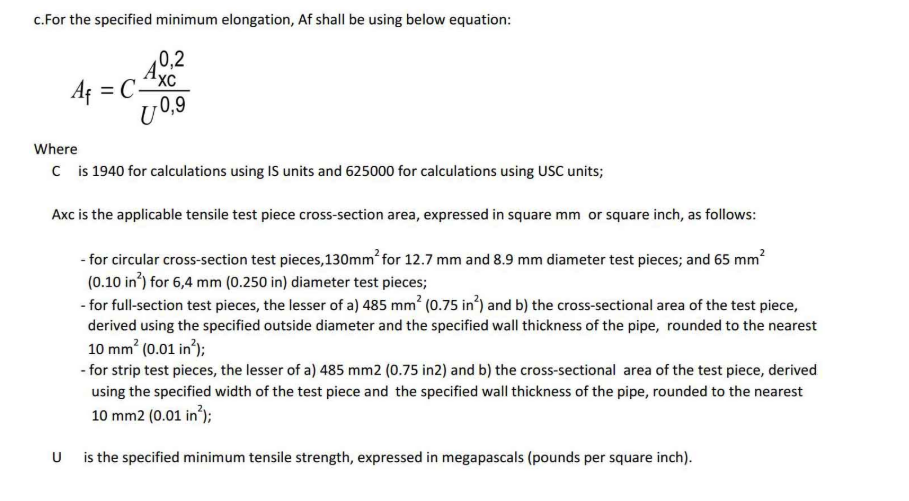
a. Cu ≤ 0,50 %; Ni≤ 0,50 %; Cr ≤ 0,50 % and Mo ≤ 0.15% b. For each reduce of 0.01% Carbon Max, an increase of 0.05% of maximum Mn is permited, up to a maximum of 1.65for grade≥ B or L245, but ≤ X52 or L360; Up to max 1.75% for grades above L360 or X52, but below L485 or X70;And up to 2.00% max for grade X70 or L485. c. Unless otherwise agreed, Nb + V ≤ 0.06%. d. Nb +V+Ti≤0.15%. e. Unless otherwise agreed. f. Unless otherwise agreed, Nb + V + Ti≤0.15%. g. B shall be not added in on purpose, and maximum B is 0.001%. | ||||||||
API 5L X46 L320 Mechanical Properties
API 5L PSL 1 pipe Mechanical propertiesTensile strength, Yeild strength, Elongation | ||||
Pipe Steel Grade | Pipe Body Of Seamless Pipe | Weld seam of EW, LSAW,SSAW and COW pipes | ||
Yield Strength | Tensile Strength | Elongation(On 50mm or 2 In | Tensile Strength | |
| Rt0.5 | Rm | Af | Rm | |
Mpa(psi),min | Mpa(psi),min | % Minimum | Mpa(psi),min | |
L175 or A25 | 175 (25 400) | 310 (45 000) | c | 310 (45 000) |
L175P or A25P | 175 (25 400) | 310 (45 000) | c | 310 (45 000) |
L210 or A | 210 (30 500) | 335 (48 600) | c | 335 (48 600) |
L245 or B | 245 (35 500) | 415 (60200) | c | 415 (60200) |
L290 or X42 | 290 (42 100) | 415 (60200) | c | 415 (60200) |
L320 or X46 | 320 (46400) | 435 (63100) | c | 435 (63100) |
L360 or X52 | 360 (52200) | 460 (66700) | c | 460 (66700) |
L390 or X56 | 390 (56600) | 490 (71100) | c | 490 (71100) |
L415 or X60 | 415 (60200) | 520 (75400) | c | 520 (75400) |
| L450 or X65 | 450 (65300) | 535 (77600) | c | 535 (77600) |
| L485 or X70 | 485 (70300) | 570 (82700) | c | 570 (82700) |
api 5l grade x46 pipe
API 5L X46 PSL2 vs PSL1 Comparision
| API 5L PSL1 vs PSL2 Pipe Differences Summary | ||
| Parameter | PSL 1 | PSL 2 |
| Grade Range | A25 through X70 | B through X80 |
| Size range | 0.405 through 80 | 4.5 through 80 |
Type of Pipe Ends | Plain-end, threaded-end; belled-end; special coupling pipe | Pained End |
Seam Welding | All methods; continuous welding limited to Grade A25 | All methods except continuous and laser welding |
Electric welds: welder frequency | No minimum | 100khz minimum |
Heat treatment of electric welds | Required for grades > X42 | Required for all grades(B through X80) |
Chemistry: max C for seamless pipe | 0.28% for grades ≥ B | 0.24% |
Chemistry: max C for welded pipe | 0.26% for grades ≥ B | 0.22% |
Chemistry: max P | 0.030% for grades ≥A | 0.025% |
Chemistry: max S | 0.030% | 0.015% |
Carbon Equivalent: | Only when purchaser specifiesSR18 | Maximum required for each grade 4.2; 4.3; 6.1.3; SR15.1 |
Yield Strength, Maximum | None | Maximum for each grade |
UTS, Maximum | None | Maximum for each grade |
Fracture Toughness | None required | Required for all grades |
Nondestructive inspection of seamless | Only when purchaser specifies SR4 | SR4 mandatory |
Repair by welding of pipe body, plate,and skelp | Permitted | Prohibited |
Repair by welding of weld seams with-out filler metal | Permitted by agreement | Prohibited |
Certification | Certificates when specified per SR15 | Certificates (SR15.1) mandatory |
Traceability | Traceable only until all tests arepassed, unless SR 15 is specified | Traceable after completion oftests (SR15.2) mandatory |
You'll find that API 5L PSL1 and PSL2 line pipe differ in several key ways. For API 5L X46 (L320) PSL2, you get tighter limits on maximum chemical content compared to PSL1, and the mechanical strength requirements are also more strictly controlled. As a spiral welded pipe manufacturer, you benefit from these differences because your production process lets you consistently meet the stricter chemistry and strength requirements of PSL2 — giving you a clear advantage in supplying higher-spec pipe to your customers.
API 5L X46 PSL2 Chemical Composition
| Steel Grade | Mass fraction, based upon heat and product analyses | Carbon | |||||||||
% maximum | % maximum | ||||||||||
Cb | Si | Mn b | P | S | V | Nb | Ti | Other | CEiiw | CEpcm | |
Welded Pipe | |||||||||||
L245M or BM | 0.22 | 0.45 | 1.20 | 0.025 | 0.015 | 0.05 | 0.05 | 0.04 | e,l | 0.43 | 0.25 |
L290M or X42M | 0.22 | 0.45 | 1.30 | 0.025 | 0.015 | 0.05 | 0.05 | 0.04 | e,l | 0.43 | 0.25 |
L320M or X46M | 0.22 | 0.45 | 1.30 | 0.025 | 0.015 | 0.05 | 0.05 | 0.04 | e,l | 0.43 | 0.25 |
| L360M or X52M | 0.22 | 0.45 | 1.40 | 0.025 | 0.015 | d | d | d | e,l | 0.43 | 0.25 |
L390 or X56M | 0.22 | 0.45 | 1.40 | 0.025 | 0.015 | d | d | d | e,l | 0.43 | 0.25 |
L415M or X60M | 0.12f | 0.45f | 1.6f | 0.025 | 0.015 | g | g | g | h,l | 0.43 | 0.25 |
L450 or X65M | 0.12f | 0.45f | 1.6f | 0.025 | 0.015 | g | g | g | h,l | 0.43 | 0.25 |
L485M or X70M | 0.12f | 0.45f | 1.7f | 0.025 | 0.015 | g | g | g | h,l | 0.43 | 0.25 |
L555M or X80M | 0.12f | 0.45f | 1.85f | 0.025 | 0.015 | g | g | g | i,l | 0.43 | 0.25 |
L625 or X90M | 0.10 | 0.55f | 2.1f | 0.02 | 0.010 | g | g | g | i,l | - | 0.25 |
L690M or X100M | 0.10 | 0.55f | 2.1f | 0.020 | 0.010 | g | g | g | i,l | 0.25 | |
L830M orX120M | 0.10 | 0.55f | 2.1f | 0.020 | 0.010 | g | g | g | i,l | 0.25 | |
a. Based upon product analysis. For seamless pipe with t> 20,0 mm (0.787 in), the CE limits shall be as agreed.
b. For each reduction of 0,01 % below the specified maximum for C, an increase of 0,05 % above the specified maximum for
permissible, up to a maximum of 1,65 % for grades ≥ L245 or B, but ≤ L360 or X52; up to a maximum of 1,75 % for grades >X52, but < L485 or X70; up to a maximum of 2,00 % for grades ≥ L485 or X70, but ≤ L555 or X80; and up to a maximum of grades> L555 or X80.
The CElIW limits apply if C> 0,12 % and the CEPcm limits apply if C ≤ 0,12 %.
c. Unless otherwise agreed, Nb + V ≤ 0,06 %.
d. Nb +V+Ti≤0,15 %.
e. Unless otherwise agreed, Cu ≤ 0,50 %; Ni ≤ 0,30 %; Cr ≤ 0,30% and Mo ≤ 0,15 %.
f. Unless otherwise agreed.
g. Unless otherwise agreed, Nb + V+ Ti ≤ 0,15 %.
h. Unless otherwise agreed, Cu ≤ 0,50 %; Ni ≤ 0,50 %; Cr ≤ 0,50% and Mo ≤ 0, 50 %.
i. Unless otherwise agreed, Cu ≤ 0,50 %; Ni ≤ 1,00 %; Cr ≤ 0,50% and Mo ≤ 0, 50 %.
j.B ≤ 0,004 %.
k. Unless otherwise agreed, Cu ≤ 0,50 %; Ni ≤ 1,00 %; Cr ≤ 0,55% and Mo ≤ 0, 80 %.
l. For all PSL 2 pipe grades except those grades to which footnote j already applies, the following applies.
Unless otherwise agreed no intentional addition of B is permitted and residual B ≤ 0,001%.
API 5L X46 PSL2 Tensile Strength, Yield Strength
API 5L PSL 2 Pipe Mechanical PropertiesTensile Strength, Yield Strength, Elongation | |||||||
| Pipe Steel Grade | Pipe body of seamless and welded pipes | Weld Seam of HFW,SAW and COW Pipes | |||||
Yield strength a | Tensile strength a | Ratio ac | Elongation (on50 mm or 2 in) | Tensile strength d | |||
Rt0.5 | Rm | Rt0.5/Rm | Af | Rm | |||
Mpa(psi) | Mpa(psi) | % | Mpa(psi) | ||||
minimum | maximum | minimum | maximum | maximum | minimum | minimum | |
L245R or BR L245N or BN L245Qor BQ L245M or BM | 245 (35 500) | 450e (65 300) e | 415(60200) | 655 (95 000) | 0.93 | f | 415(60200) |
L290R or X42R L290N or X42NL290Qor X42Q L290M or X42M | 290 (42100) | 495 (71800) | 415(60200) | 655(95000) | 0.93 | f | 415(60200) |
L320N or X46NL320Q or X46QL320M or X46M | 320(46 400) | 525(76100) | 435(63 100) | 655 (95 000) | 0.93 | f | 435(63 100) |
L360N or X52NL360Q or X52Q L360M orX52M | 360(52200) | 530(76900) | 460(66700) | 760(110200) | 0.93 | f | 460(66700) |
L390N or X56NL390Qor X56Q L390M or X56M | 390(56 600) | 545(79 000) | 490(71 100) | 760(110 200) | 0.93 | f | 490(71100) |
L415N orX6ON L415Q or X60Q L415M or X60M | 415(60200) | 565(81900) | 520(75400) | 760(110200) | 0.93 | f | 520(75 400) |
L450Q or X65QL450M or X65M | 450(65 300) | 600(87000) | 535 (77 600) | 760(110200) | 0.93 | f | 535(77600) |
L485Q or X70Q L485M or X70M | 485(70 300) | 635(92100) | 570(82 700) | 760(110200) | 0.93 | f | 570(82700) |
L555Q or X80Q L555M or X80M | 555(80500) | 705(102 300) | 625(90600) | 825(119 700) | 0.93 | f | 625(90 600) |
L625M or X90M | 625(90600) | 775 (112 400 | 695 (100800) | 915 (132700) | 0.95 | f | 695(100 800) |
L625Q or X90Q | 625(90 600) | 775(112 400) | 695(100 800) | 915(132 700) | 0.97h | f | 695(100800) |
L690M or X100M | 690b (100100)b | 840b (121 800)b | 760(110200) | 990(143 600) | 0.97h | f | 760(110200) |
L690Q or X100Q | 690 b (100100)b | 840b (121800)b | 760(110200) | 990(143 600) | 0.97h | f | 760(110200) |
| L830M or X120M | 830b (120 400) b | 1050b (152 300)b | 915(132700) | 1145(166 100) | 0.99h | f | 915(132 700) |
API 5L X46 Pipe Pressure Rating (Mechanical Strength)
You will find that the minimum yield strength of API 5L X46 (i.e. L320 pipeline pipe) is 46400 psi (320 MPa), which is why we call it X46 or L320 grade. Its tensile strength is 63100 psi (435 MPa). The performance of X46 is superior to X42 and B-class, therefore it is in high demand in the oil and gas industry.
Whether it is seamless pipe or welded pipe (ERW, LSAW), the pressure rating, tensile strength, and yield strength of X46 pipes are the same. If the working conditions require higher pressure, you must increase the wall thickness of the steel pipe or choose a higher steel grade from API 5L.
As a spiral welded pipe factory, when the project requires a larger wall thickness or higher pressure rating, you can flexibly adjust the wall thickness and steel grade through the spiral welded pipe process. While ensuring the consistency of mechanical properties of X46 and even higher grades, you can quickly meet the large-scale demand for high-strength pipeline pipes in the oil and gas industry.
Testing Items
In the quality control of pipeline pipes, you will encounter several key tests, each of which is directly related to the safety and reliability of the pipeline under actual working conditions.
Bending test: You need to confirm that there should be no cracks in any part of the sample or weld opening.
Flattening test: This is a test used to demonstrate the deformation performance of pipelines. It should demonstrate resistance to longitudinal and circumferential cracking, including internal and external defects. You should note that this test is applicable to ERW pipes with a diameter exceeding 12.75 inches; For pipelines with OD/WT>10, the weld seam must not have openings until the distance between the plates is less than 30% of the original outer diameter.
Guided bending test: You should pay attention to the situation of complete fracture - any crack or rupture in the weld metal with a length exceeding 3.2mm should be displayed, regardless of depth; Or exposed to the base material, heat affected zone, or fusion line, with a length exceeding 3.2mm or a depth exceeding 12.5% of the wall thickness.
Water pressure test: You need to conduct a 100% water pressure test, requiring that the weld seam or pipe body has no leakage. If the pipe section used has already been successfully tested, the connection or joint does not need to undergo hydrostatic pressure testing again.
CVN impact test: This is the test required for PSL2 tubes. Seamless pipes should be tested together with the pipe body, while welding tests include pipe body, weld seam, and heat affected zone tests. The usual temperature for impact testing is 0 ℃.
DWT test: This is the test that needs to be conducted on the PSL2 pipeline.
These experiments may sound demanding, but what really matters to you is who will test them, where they will be tested, and whether the data is reliable. Wuzhou brand has its own CNAS accredited laboratory, which means that the bending, flattening, guided bending, water pressure, CVN impact, and DWT tests mentioned above can all be completed according to standards in Wuzhou factory, and the test results are authoritative and traceable. You don't have to send samples back and forth, nor do you have to worry about the testing cycle slowing down the delivery time - from raw materials to finished products, Wuzhou helps you control every quality link in your own hands, giving you not only a qualified spiral welded pipe, but also a visible and traceable quality assurance.
WU ZHOU Supply Ranges And Sizes
API SPECS 5L Gr. X46 or L320
Standard: API 5L, ISO 3183
Grade: X46 or L320 (Suffix letter N, Q, M, R)
SSAW pipe Outerdiameter: 219mm – 3620mm, 8” – 144”
Wall Thickness: 6-25.4mm
Pipe Thickness Schedule: SCH 20, SCH 30, SCH STD, SCH40, SCH60, SCH XS, SCH 80, SCH 100, SCH 120, SCH 140, SCH XXS of the standard thickness
Range of Length: SRL, DRL, 5 meter to 30 meter
Fixed Length: 5.8 Meter, 6.0 Meters (20FT), 11.8 Meters, 12.0 Meters (40FT)
Product Specification Level: PSL1, PSL2, Sour
Ends: Plain, Beveled Ends, Threaded Ends
Available Coating: Black Painting, Varnished, Anti-Rust Oil, FBE, 3PE/3LPE, 3PP, Galvanized
Certification

You need a product



You May Like


- Nearest port for product export
- Tianjin Port, Port of Tangshan
- Delivery clauses under the trade mode
- FOB, CFR, CIF, EXW, FCA
- Acceptable payment methods
- T/T, L/C